Xometry FAQ: No-Nonsense Answers on CNC Materials, Reaming Wood, Tool Holder Torque & More
-
Xometry FAQ: Straight Answers for Engineers & Buyers
-
1. What exactly is the Xometry official homepage and what can I actually do there?
-
2. Is the range of "Xometry CNC materials" as wide as it seems?
-
3. Wait, can I really ream wood on a CNC? What about a reamer for wood?
-
4. What about a "VMC Jamaica Hibiscus Cocktail"? Is that a real thing?
-
5. How tight should my tool holder be for a job on a CNC machine?
-
6. One last thing: Is the Xometry instant quoting engine really accurate?
-
1. What exactly is the Xometry official homepage and what can I actually do there?
Xometry FAQ: Straight Answers for Engineers & Buyers
You've got questions about Xometry. Maybe you're wondering what materials are available for a CNC part, how to handle a weird reaming job on wood, or if that instant quote is too good to be true. I deal with these questions every day—usually when someone's on a tight deadline and their usual vendor fell through.
Here's what I've learned from triaging hundreds of rush orders and testing (and failing with) various approaches on their platform. No fluff, just answers to the stuff that actually matters.
1. What exactly is the Xometry official homepage and what can I actually do there?
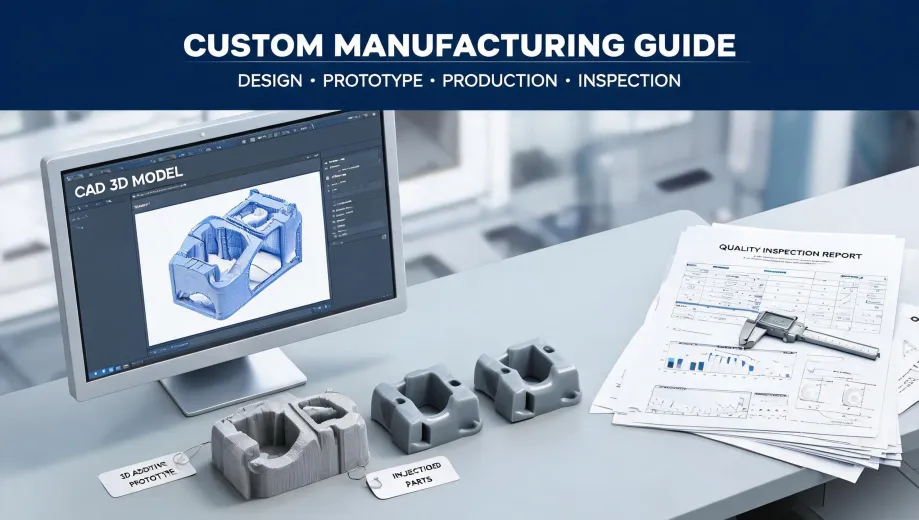
It's tempting to think it's just a quoting tool. But the Xometry homepage (xometry.com) is the command center for their on-demand manufacturing platform. You can upload a CAD file, get an instant quote for CNC machining, 3D printing, injection molding, or sheet metal, and place an order immediately. That's the core.
But what I've learned from using it in a pinch is to check a few specific things:
- The Material Library: They don't just list them; they show you comparative properties and lead times for different grades of aluminum, steel, and plastics. This is gold when you're swapping a material last minute.
- The DFM Feedback: The instant quote engine often flags design-for-manufacturing issues before you order. I ignored this once (assumption failure) assuming I knew better. Turned out the automated analysis caught a wall thickness issue I'd missed. It saved a $4,000 order from being scrapped. (Note to self: always check the DFM report.)
2. Is the range of "Xometry CNC materials" as wide as it seems?
Yes, and it's more nuanced than a simple list. You can pick from dozens of options, from standard 6061 Aluminum to more exotic stuff like PEEK or Invar. But here's the reality: just because a material is in the dropdown doesn't mean it's the best choice for your specific geometry or lead time.
What was best practice in 2022 may not apply in 2025. Five years ago, you'd often have to call to confirm stock for specialty materials. Now, the platform shows real-time availability and lead times for each material.
The 'pick whatever is cheapest' advice ignores the fact that some materials require specific tooling or post-processing. I once assumed a tougher aluminum alloy would just cost a bit more. Didn't verify the machining time difference. Turned out the harder material doubled the cycle time and blew my budget. The instant quoting engine can't always predict that internal complexity, so it pays to understand the trade-off between material properties and machinability.
3. Wait, can I really ream wood on a CNC? What about a reamer for wood?
Ah, this is a classic. Yes, you can ream wood, but it's not like reaming metal. The term "reamer wood" often gets thrown around, but the correct tool for a clean, accurate hole in wood on a CNC is usually a spiral router bit or a dedicated wood boring bit, not a standard metal reamer.
I discovered this the hard way (communication failure). I said I needed a "reamed hole" in a machined wood part for a prototype. The vendor heard "use a standard metal reamer." Result: a torn, fuzzy hole that looked nothing like what I'd designed. The fundamentals haven't changed—you need a sharp, properly ground tool—but the execution is completely different for wood vs. metal.
If you're specifying this on Xometry for a wood prototype, specify the tool path and finish requirements explicitly. Don't rely on the generic term "reaming."
4. What about a "VMC Jamaica Hibiscus Cocktail"? Is that a real thing?
Honestly, this is a left-field search term. A VMC (Vertical Machining Center) isn't making drinks. But it gives me a perfect opportunity to talk about a real-world scenario. A client once needed a custom stainless steel jigger for a cocktail competition. It had a complex, thin-walled design for a hibiscus syrup mixing tool. The question wasn't just "can you make it?" but "can you make it with the right surface finish and tolerance for a food-grade, aesthetic application on a VMC?"
The numbers pointed toward a cheaper 3D-printed prototype. My gut said go with a machined part for the finish and durability. I went with a CNC prototype on Xometry. It cost $180 more, but it perfectly matched the client's vision. The alternative was a $2,000 custom injection mold and a lot of disappointment. Moral of the story: know when the machine tool isn't the right analogy for the product, but also know when the precision of that tool is exactly what you need.
5. How tight should my tool holder be for a job on a CNC machine?
This is the technical question every machinist struggles with at some point. The simple advice is "tight enough to hold the tool without slipping, but not so tight you damage the holder or the tool." But (ugh) that's uselessly vague.
Every spreadsheet analysis pointed to a specific foot-pound value. Something felt off. Turns out the recommended torque for a standard ER collet is often lower than you'd think to avoid collapsing the collet. Over-tightening is a classic mistake. I learned this after a job where a tool slipped and ruined a part. The machine's spindle load was fine, but the tool holder wasn't gripping properly due to excessive or uneven torque.
For most standard steel tool holders and collets, 30-40 foot-pounds is a good starting point for a 1/2" shank tool. But you must use a torque wrench. "Finger tight plus a grunt" isn't a standard. Trust me, it's a $50 wrench that saves a $500 part. As a general rule, use a pull-stud retention force that matches the machine manufacturer's spec—usually over 2,000 lbs for a 40-taper spindle.
6. One last thing: Is the Xometry instant quoting engine really accurate?
The 'it's just a rough estimate' advice is outdated. In my experience, the quotes from Xometry are surprisingly accurate for standard geometries and common materials. They're now a benchmark for pricing in our industry. But they do not include every potential hidden cost for complex or highly iterative parts.
This was true 5 years ago when digital quoting was new. Today, the engine is sophisticated. But I always add a 15-20% buffer for secondary operations (like intricate surface finishing or tight tolerances on non-standard planes). The instant quote is a fantastic starting point, not a final contract.
Prices as of today for a simple 6061 aluminum part are typically in the $50-150 range for low quantity (1-5 units), but this varies wildly. Verify current rates for your specific CAD file.